Skip to content

2026 Best Checkweigher Online for Global Buyers?

Choosing the 2026 Best Checkweigher Online for Global Buyers is not just a matter of comparing prices. A suitable machine must match the product, production speed, and weighing range on your line. A small sachet and a heavy carton create different demands. Details matter.

This guide explains how to assess a Checkweigher Online before requesting a quotation. Compare stated weighing accuracy, belt dimensions, throughput, and the size range the system can handle. Ask how the machine connects with your existing conveyor, packaging equipment, and production records. A clear product page helps, but it cannot replace a practical review of your actual packages and operating conditions.

Look beyond the headline specifications. Request sample test results, calibration documentation, installation guidance, and details about spare parts and technical support. For international orders, confirm delivery terms, commissioning options, language support, and service coverage in your region. Requirements can vary by industry and destination, so buyers should verify applicable standards with the supplier and relevant local experts.

A polished listing may still omit an important limitation. It is easy to focus on advertised speed and overlook changeover time or cleaning access. Ask direct questions, and request a demonstration using representative products when possible. This guide is intended to help buyers compare options more carefully—not to declare one model best for every factory.
2026 Best Checkweigher Online for Global Buyers?

Define Checkweighers and Their 3 Core Weighing Functions

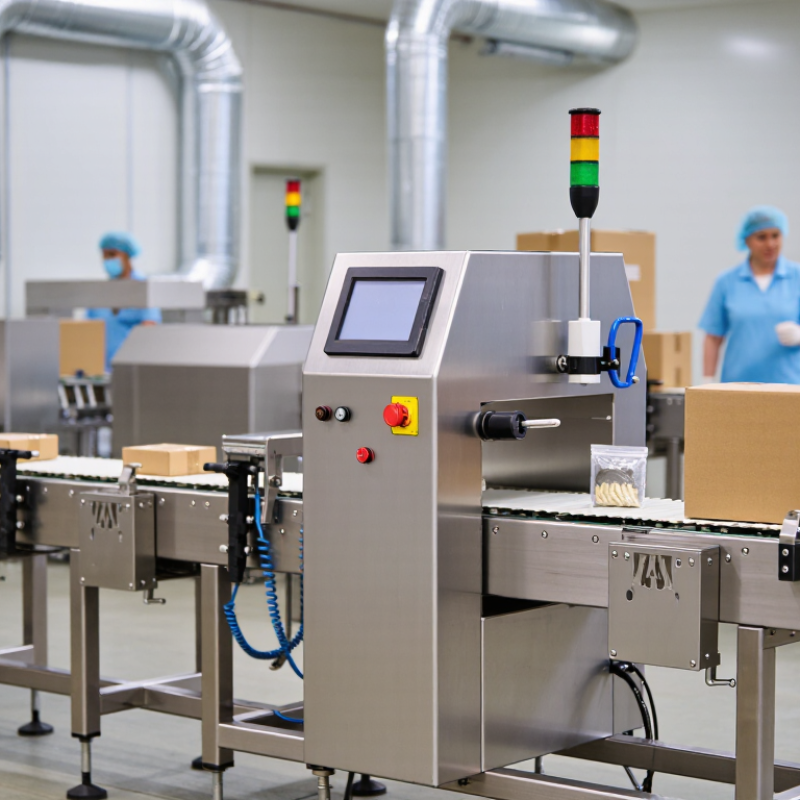
A checkweigher is an in-line weighing system that measures products as they move along a conveyor. Unlike a bench scale, it must capture a stable weight during a brief pass. Each reading depends on correct setup, steady product spacing, and suitable line speed. Small cartons, flexible pouches, and vibrating conveyors can behave differently.

Its first core function is dynamic weighing: a load cell records each item’s weight while it crosses the weighing section. The second is checking that result against a target weight and configured upper and lower limits. A product inside the permitted range passes; one outside it is flagged. Not magic. Poorly placed guides or changing belt speed can distort readings, so installation and routine verification matter.

The third function is handling and documenting out-of-range items. Depending on the line, the system may trigger a pusher, air blast, stop signal, or operator alert. It can also store weight results and show trends, helping teams notice gradual changes before many packages are affected. A reject mechanism still needs practical checks: a missed or full collection bin can undermine good measurements. Operators should confirm that the weighing setup matches the actual product and production conditions.

Compare OIML R 51-1:2006 Classes X and Y

For global buyers comparing online checkweighers, OIML R 51-1:2006 offers a practical starting point. The recommendation defines two main accuracy classes: X and Y. Class X uses a numerical factor alongside the class designation, while Class Y uses named subclasses, including Y(a), Y(b), and Y(I) through Y(IIII). These labels are not interchangeable. They indicate different performance requirements for automatic weighing applications.

Check the full designation, not just the headline class. OIML R 51-1:2006 assesses performance across load conditions and during automatic operation; a single static accuracy figure cannot tell the whole story. Ask for test results at your intended product weight and line speed. For example, a line weighing small sealed packs at high throughput may face different practical challenges from one handling heavier cartons slowly. Keep the setup realistic. The OIML document is a technical recommendation, not a market survey, so compare its requirements with measured results from the actual installation. A class label alone can mislead. Dust, vibration, product spacing, and belt changes may affect repeatability, and these details deserve careful review.

2026 Best Checkweigher Online for Global Buyers? Compare OIML R 51-1:2006 Classes X and Y

OIML R 51-1:2006 identifies two principal accuracy-class designations: X and Y.

How to read this chart: Each bar represents one principal class designation, not a measurement of accuracy. The chart does not indicate that either class is more accurate. Check the applicable subclass, instrument approval, intended application, and local legal-metrology requirements when selecting a checkweigher.

Assess Capacity, Throughput, and Scale Intervals d and e

Choosing an online checkweigher starts with the product, not the headline speed. Record the lightest and heaviest packs, including trays and labels, then compare that range with the machine’s usable capacity. A unit rated for a generous maximum load may still struggle with tiny products or abrupt weight changes. Leave a sensible margin; operating constantly near the limit can make results less stable.

Throughput depends on more than packs per minute. Product spacing, belt speed, pack shape, and vibration all affect how consistently each item is weighed. Ask for performance data using products and line conditions close to your own. A fast test with evenly spaced cartons may not reflect a crowded shift. Small details matter. It is worth admitting that line speed estimates are often optimistic.

Check the scale intervals carefully. “d” commonly refers to the displayed scale interval, while “e” refers to a verification interval used in applicable metrological assessments. Their meaning and permitted use can depend on the instrument and intended application. Do not assume a smaller d alone guarantees better weighing performance. Review the specification sheet, confirm how the equipment handles your product range, and clarify which interval applies to your installation. A short sample trial can reveal problems that a neat table misses.

Check EU MID 2014/32/EU MI-006 and Local Approvals

For global buyers, a checkweigher’s speed and accuracy are only part of the decision. If it is used for legally controlled weighing, confirm whether it falls under EU Directive 2014/32/EU, Annex MI-006, for automatic weighing instruments. Details matter. A machine used for internal process checks may face different requirements from one used to determine a traded quantity. Ask the supplier for the intended-use statement, conformity documents, and the exact model configuration covered. A changed conveyor, software setting, or load cell can affect the assessment.

Do not assume EU conformity settles every local requirement. Before ordering, check with the destination country’s legal metrology authority or a qualified local specialist. Rules may involve national registration, in-service verification, inspection intervals, or language requirements. Keep records of the instrument’s markings, serial number, test results, and installation conditions. A practical check is to run sample packs at the actual line speed and retain the results. Paperwork helps. So does a witnessed test. One detail is easy to miss: approval for a device does not always confirm that its installation or use is acceptable locally. Verify both before shipment, and document any uncertainty rather than treating it as settled.

Select a Supplier Using FAT, Calibration, and Service Criteria

2026 Best Checkweigher Online for Global Buyers?

Choosing a checkweigher supplier takes more than comparing speed and quoted accuracy. Ask for a Factory Acceptance Test (FAT) using products close to your actual packs. Record line speed, reject timing, weight variation, and changeover steps. A useful FAT report shows test conditions, sample counts, and results—not only a pass mark. Check that installation plans cover conveyor height, utilities, and integration with upstream equipment. Small details matter.

Calibration needs clear intervals, traceable reference weights, and documented procedures. Confirm who performs calibration, what certificates are supplied, and how deviations are handled. A certificate alone does not prove stable performance on your line. Request an on-site verification after installation, then compare routine check results over time. Service access matters too. Ask about response hours, spare-part availability, remote diagnostics, and technician coverage in your region. Get these commitments in writing. Sales promises can sound reassuring; I would still test the escalation process before signing.

Tips: Send sample products and packaging data before the FAT. Agree on acceptance limits and reject tests in advance. Keep one awkward product in the trial; real lines are rarely perfect. If support coverage is vague, pause and ask again.

2026 Best Checkweigher Online for Global Buyers? - Select a Supplier Using FAT, Calibration, and Service Criteria

Evaluation area What to compare Evidence to request Buyer guidance
Product and weighing range Minimum and maximum package weight, package dimensions, product type, and conveyor requirements. A written specification showing the validated weighing range and any product or package limitations. Confirm that the intended product range is within the system’s specified operating range; do not select by maximum capacity alone.
Throughput and weighing performance Required packages per minute, product spacing, line speed, and acceptable weighing error for each product. A performance proposal stating the test conditions, sample product, target speed, and agreed acceptance limits. Throughput and accuracy depend on product characteristics, spacing, vibration, and installation. Require testing with representative products at the intended operating conditions.
FAT scope and acceptance Functional checks, reject operation, alarms, data logging, recipe changes, and performance testing. An agreed Factory Acceptance Test (FAT) protocol, recorded results, test conditions, and a list of open issues. Define pass/fail criteria before ordering. A FAT should test agreed functions and representative products; it does not replace site acceptance testing.
Calibration and traceability Calibration method, reference weights, documentation, and how performance checks will be repeated on site. Calibration records identifying the equipment and results; where required, evidence of traceability to recognized measurement standards. Calibration of the weighing system is distinct from dynamic production performance testing. For calibration services, check whether the laboratory’s accreditation covers the relevant measurement scope.
Legal metrology requirements Whether the application is subject to regulated weighing or prepackage control in the destination market. Applicable approvals, conformity documents, and instructions for verification in the target jurisdiction. Requirements vary by country and application. OIML R 51 addresses automatic catchweighing instruments, but buyers should confirm local rules with the relevant authority or qualified local specialist.
Reject system and line integration Reject-device type, reject confirmation, reject-bin monitoring, line stops, and interfaces with upstream or downstream equipment. An integration and risk-control description, interface list, and FAT test results for reject and fault conditions. Confirm that rejected products are detected and handled as intended, including when the reject device fails or the collection bin is full.
Hygiene and environmental protection Cleaning method, washdown exposure, dust, temperature, and contact-material requirements for the application. Declared ingress-protection rating, cleaning instructions, material details, and any relevant food-contact documentation. IP ratings are defined by IEC 60529; confirm the exact rating and what it covers. Choose construction and cleaning provisions to suit the actual process rather than relying on a general “washdown” description.
Data, records, and connectivity Production reports, user access, recipe control, data export, and required connection to plant systems. A confirmed interface list, sample reports, data-retention details, and a demonstration using the buyer’s intended workflow. Specify the required data fields and interfaces in the purchase documents. Verify compatibility with the actual plant network and software environment.
Installation and commissioning Site preparation, installation responsibility, operator training, commissioning checks, and handover documentation. A commissioning plan, site utility requirements, training agenda, and completed handover checklist. Agree who provides labor, utilities, product samples, and line access, and define how site acceptance will be documented.
Service and spare parts Support hours, remote troubleshooting, local service coverage, spare-parts availability, and escalation process. Written service terms, parts list, warranty conditions, and any contractual response or restoration targets. Response times and parts availability are supplier-specific. Make required service levels contractual and confirm coverage for the installation location.
Total cost of ownership Equipment price, installation, training, calibration, consumables, maintenance, software, and expected downtime costs. An itemized quotation with exclusions, warranty terms, recurring charges, and recommended maintenance requirements. Compare suppliers using the same scope and operating assumptions, not purchase price alone.

Note: Performance values and compliance requirements are application- and jurisdiction-specific. Obtain written, product-specific commitments and verify applicable local regulations before purchase.